
The plastics and rubber industry holds a distinctive place in Morocco's industrial landscape. It supplies food packaging, automotive equipment, construction and public works, agriculture and consumer goods: bottles and caps, bumpers and dashboards, window profiles, pipes and ducts, seals, belts and retreaded tyres. Behind each of these products stand heavy lines, often run continuously, where metal is everywhere: press frames, injection moulds, extruder screws and barrels, calenders, mixers and vulcanising presses, as well as conveyors, silos, electrical cabinets and handling structures.
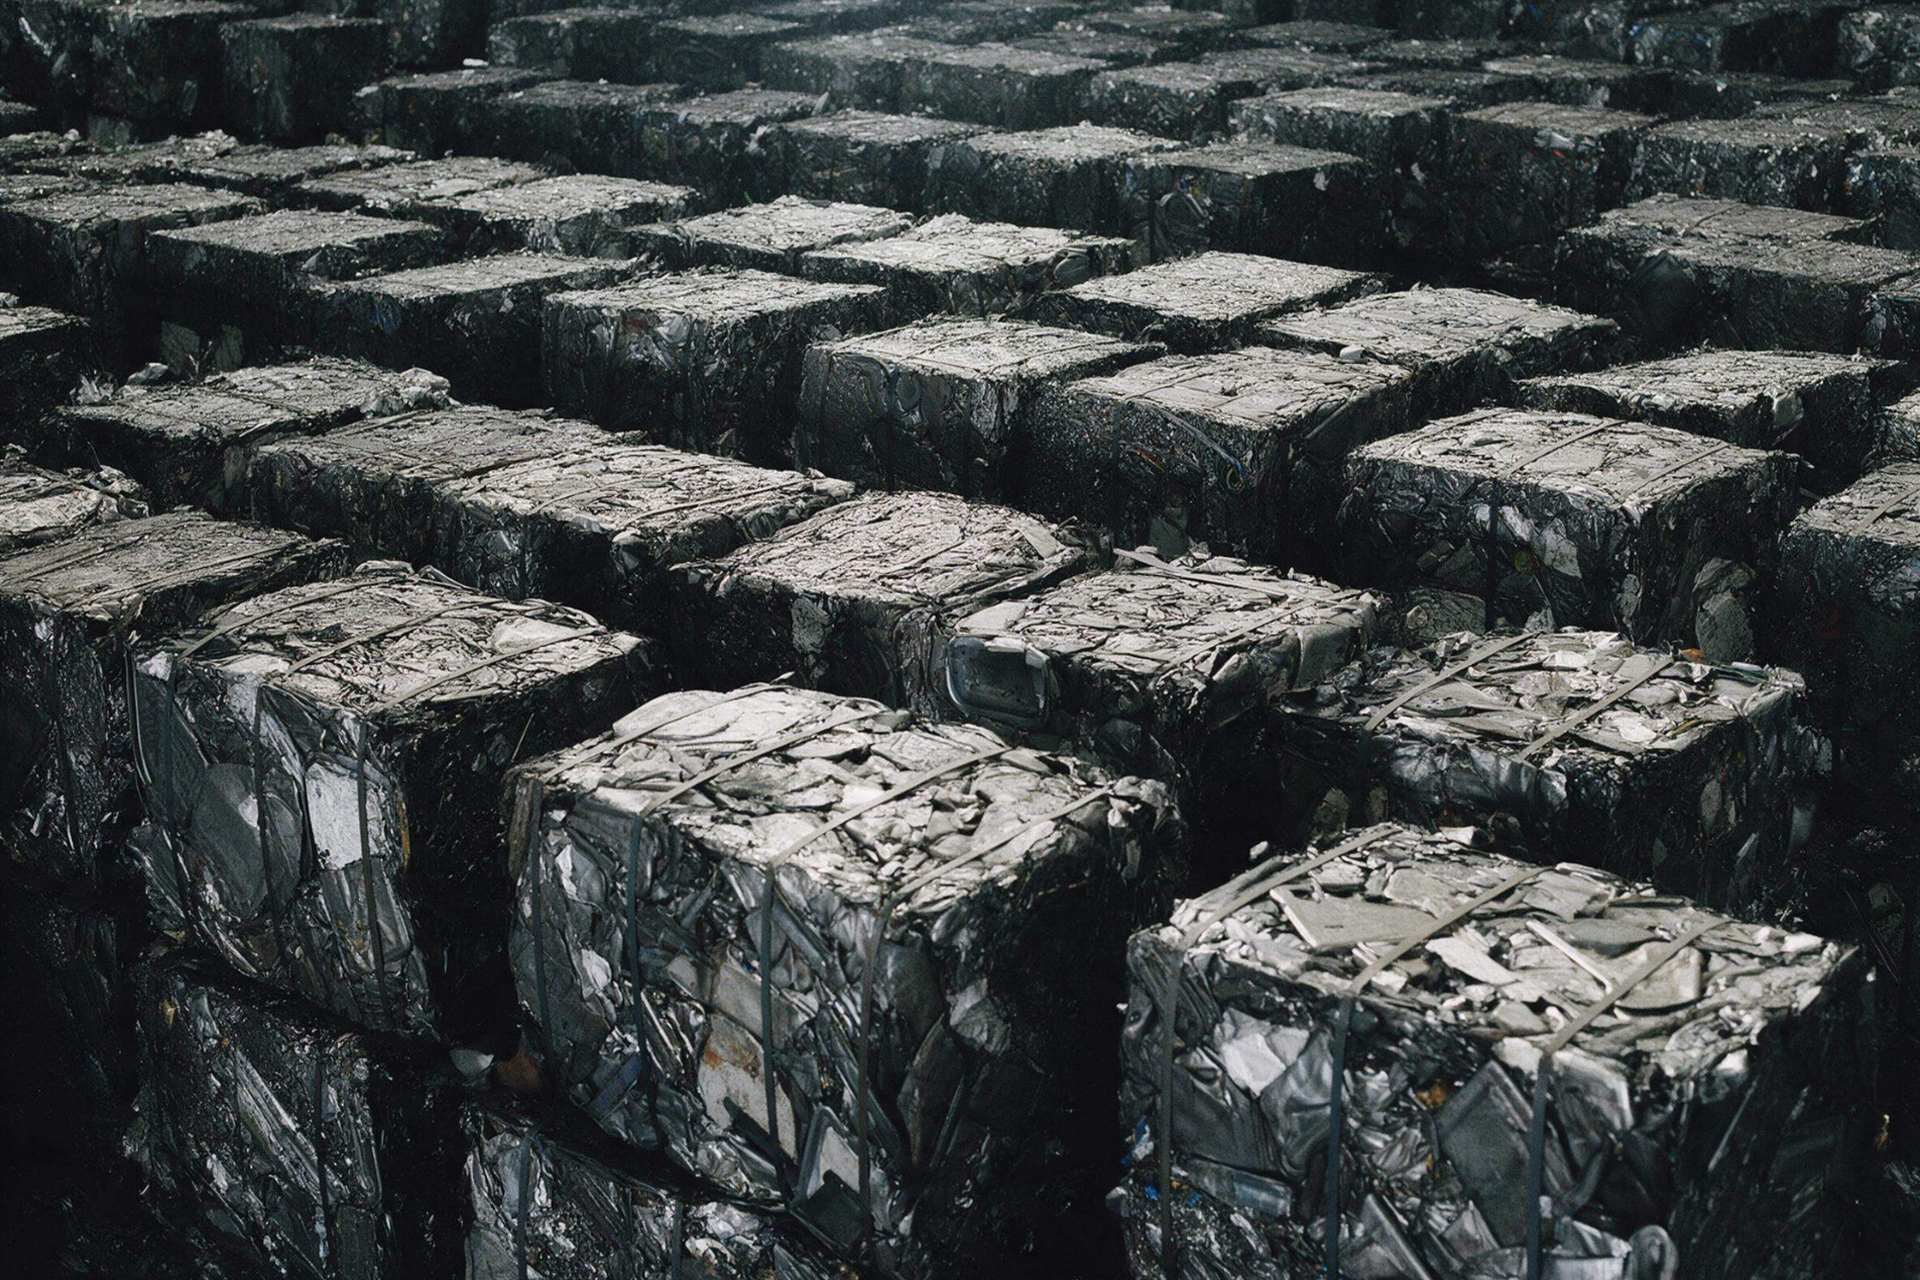
When a line changes production, when a mould reaches end of life, when a workshop moves or a plant closes, this equipment becomes a significant metal resource, provided it is dismantled, sorted and cleared away methodically. For plant directors, maintenance managers and workshop supervisors, the issue is not only freeing up space: production continuing next door must be protected, risks linked to heavy parts and fluids must be prevented, and each part must be judged — what can still be used, and what belongs to material recovery. This guide explains, in practical terms, how to approach plastics and rubber scrap metal in Morocco.
A dense industrial fabric, from Casablanca to Kenitra
Moroccan plastics processing concentrates in the Kingdom's major industrial zones. Casablanca and its outskirts — Aïn Sebaâ, Sidi Bernoussi, Berrechid — bring together long-established converters of packaging, caps and technical parts. The Kenitra automotive hub, with its suppliers settled around the free zone, produces injected, blow-moulded and extruded parts for vehicles assembled in Morocco. Tangier, with its free zones and port, hosts converters geared to export, while Agadir and Marrakech serve food processing and construction with films, pipes and profiles.
Rubber follows a similar geography: tyre retreading workshops for heavy trucks and machinery, makers of seals, belts and technical parts for industry and construction, and vulcanising workshops attached to transport fleets and mines. Each segment generates its own metals, but all share the same constraint: heavy, often bespoke equipment, installed to last, whose replacement calls for major lifting and transport resources. It is in this context that Morocco's automotive sector, a heavy consumer of plastic parts, illustrates the volumes at stake: our article on chemical and petrochemical scrap covers neighbouring process lines, and paper, cardboard and printing scrap shows the same phased approach in another Moroccan converting industry.
Moulds and tooling: the first metal resource
The mould is the central tool of plastics processing, and its most valuable metal. Multi-cavity injection moulds, blow moulds, extrusion dies and compression moulds for rubber are machined from tool steels chosen for hardness, polishability and resistance to thermal fatigue. Cavities are often hardened or surface-treated, cores and ejectors adjusted to a tenth of a millimetre, temperature-regulation circuits drilled through the heart of the blocks. A large mould can weigh several tonnes and require an overhead crane for the slightest move.
Alongside tool steels are aluminium moulds for short runs, prototypes and some blow-moulded parts, as well as stainless steels for moulds exposed to corrosive materials or damp environments. Sorting must therefore separate the families at dismantling: tool steel on one side, ordinary steel from frames and clamping plates on the other, aluminium apart, not forgetting fitted elements — hot runners, nozzles, heaters and ejection cylinders — which belong to different streams. And before any cutting, each mould deserves examination: a mould still functional, repairable or adaptable to another production can find a second life with another converter, whereas a cracked mould, out of tolerance or incompatible with current lines joins material recovery, sorted by family.
Extruders, injection presses and processing lines
Beyond moulds, the lines themselves concentrate large tonnages. An injection press combines a massive frame, mould platens, a clamping unit, hydraulic cylinders and a complete hydraulic power pack, with tank, pumps and motors. A single-screw or twin-screw extruder adds the screw and barrel — wear parts in highly alloyed steel, often coated — the hopper, the filtration system and the die head. Blow moulders, thermoformers and extrusion-blow lines complete the fleet, with their own frames, cylinders and cooling systems.
On the rubber side, equipment is just as metallic: Banbury-type internal mixers with rotors and chambers, multi-roll calenders, vulcanising presses with heated platens, rubber extruders, cutters and granulators. Around these machines sit the ancillaries that weigh in a load: reclaim crushers and granulators, dryers, dosers, conveyors, material silos, cooling tanks, chillers, compressors and electrical cabinets. Dismantling follows the reverse order of assembly, assembly by assembly, with marking and photographs, so that every element can be identified and routed to the right stream. This method follows the same principles as industrial dismantling in cement plants applied to lines where every hour of downtime counts.
The metal families to sort on site
A plastics or rubber workshop holds a more varied inventory of metals than it first appears. Tool steels dominate moulds and wear parts; alloy steels equip screws, barrels, shafts and cylinders; cast iron forms many press and calender frames; stainless steel appears in hoppers, tanks and parts in contact with food or corrosive materials; aluminium equips light moulds, housings and guard profiles; copper, finally, is present in heater bands, heating elements and cartridge heaters, motor windings, cables and electrical cabinets.
On-site sorting must separate these families before collection, and isolate elements that would disturb the batches: chrome coatings, surface treatments, hard-metal inserts, vulcanised rubber residues stuck to platens, non-metallic ducts, seals and gaskets. Electric motors, numerous on these lines, form their own stream, as do cables and cabinets. To organise this sorting, the French guide to metal sorting sets out the simple gestures — magnet, colour, weight — that let a workshop team separate streams correctly without laboratory equipment.
Safety and depollution: oils, fluids and heating elements
Plastics and rubber impose specific precautions before any cutting. The first concerns handling: a mould weighing several tonnes is not moved by hand, its centre of gravity is unpredictable once separated from the press, and its tipping can crush or sever. Only suitable lifting equipment, checked slings and a lifting plan agreed with the workshop manager allow an accident-free removal. The second concerns pressure: a press or cylinder left under hydraulic load must be isolated, depressurised and checked before any dismantling.
Depollution comes next. Hydraulic circuits and clamping units are drained before dismantling; mould temperature controllers hold heat-transfer fluids that are purged and packed separately; heater bands and heating elements, sometimes still carrying residual voltage, are disconnected and checked before handling. Spilled plastic pellets and fine, combustible dust are cleaned and vacuumed before any hot cutting, governed by a hot-work permit. Parts soiled with rubber are never hot-cut without preparation, to avoid fumes. These gestures mirror those practised in chemical and petrochemical industry scrap in Morocco, where draining and packing fluids condition every intervention.
Dismantling in phases, without stopping production
In a plastics plant, production often continues while a neighbouring line is removed. Phased work is therefore the central tool: advance inventory, marking of assemblies, removal order — peripherals first, utilities next, main line last — and planned shutdown windows for work requiring a shared utility to stop, such as a workshop power supply or a cooling-water network. Each phase ends with the area restored: floors cleaned, access cleared, guards put back.
Clearance follows the same discipline. Removed metals are gathered on storage areas set away from production flows, without blocking material reception docks or finished-product shipments, then loaded onto suitable vehicles, carefully secured. Traceability accompanies each load: type of metal, line of origin, weighing and destination, so the route followed by each family can be documented. For a relocation, dismantling stays reversible — assemblies marked, plans kept, fragile parts protected — so the line can be reassembled in the new workshop. For a permanent shutdown, phasing workshop by workshop frees surfaces gradually, without paralysing the site. Agricultural scrap and data-centre scrap show the same phased approach in other Moroccan industries.
FAQ — Plastics and rubber industry scrap metal in Morocco
Can an injection press be removed without stopping the whole workshop? Yes, in many cases, provided work is phased, the removal zone is isolated, shutdowns of shared utilities are coordinated with production, and work on shared networks only takes place during planned windows. Feasibility depends on the layout of the line, its connections and production constraints.
What happens to worn moulds, even scratched or modified ones? They are first examined for reuse or repair: a mould still within tolerance can serve another production. Otherwise they are sorted by metal family — tool steel, aluminium, fitted elements apart — before joining material recovery.
Why drain hydraulic circuits and temperature controllers before cutting? Because no liquid must remain inside a machine when it is cut or loaded: oils and heat-transfer fluids are purged, packed in closed, labelled containers and routed to suitable streams.
How should heavy moulds be handled safely? With suitable lifting equipment, checked slings, a lifting plan agreed with the workshop manager, and a clear area around the move. A mould is never moved by hand and never tipped without controlling its centre of gravity.
Can an extrusion line be relocated rather than dismantled for recovery? Yes, when the line is still in working order: dismantling is then reversible, assembly by assembly, with marking, protection of fragile parts and plans kept, so the line can be reassembled in the new workshop.
Entrust your plastics and rubber scrap to MOUMETAL
MOUMETAL supports Moroccan plastics and rubber converters with the removal, sorting and recovery of metals from their lines, from injection moulds and extruders to vulcanising presses and calenders. To organise an intervention, a site visit or a collection coordinated with your production, contact MOUMETAL on +212 660 690 806 or by email at contact@moumetal.com. To go further, see our French guides to scrap purchase and metal sorting on moumetal.com.