
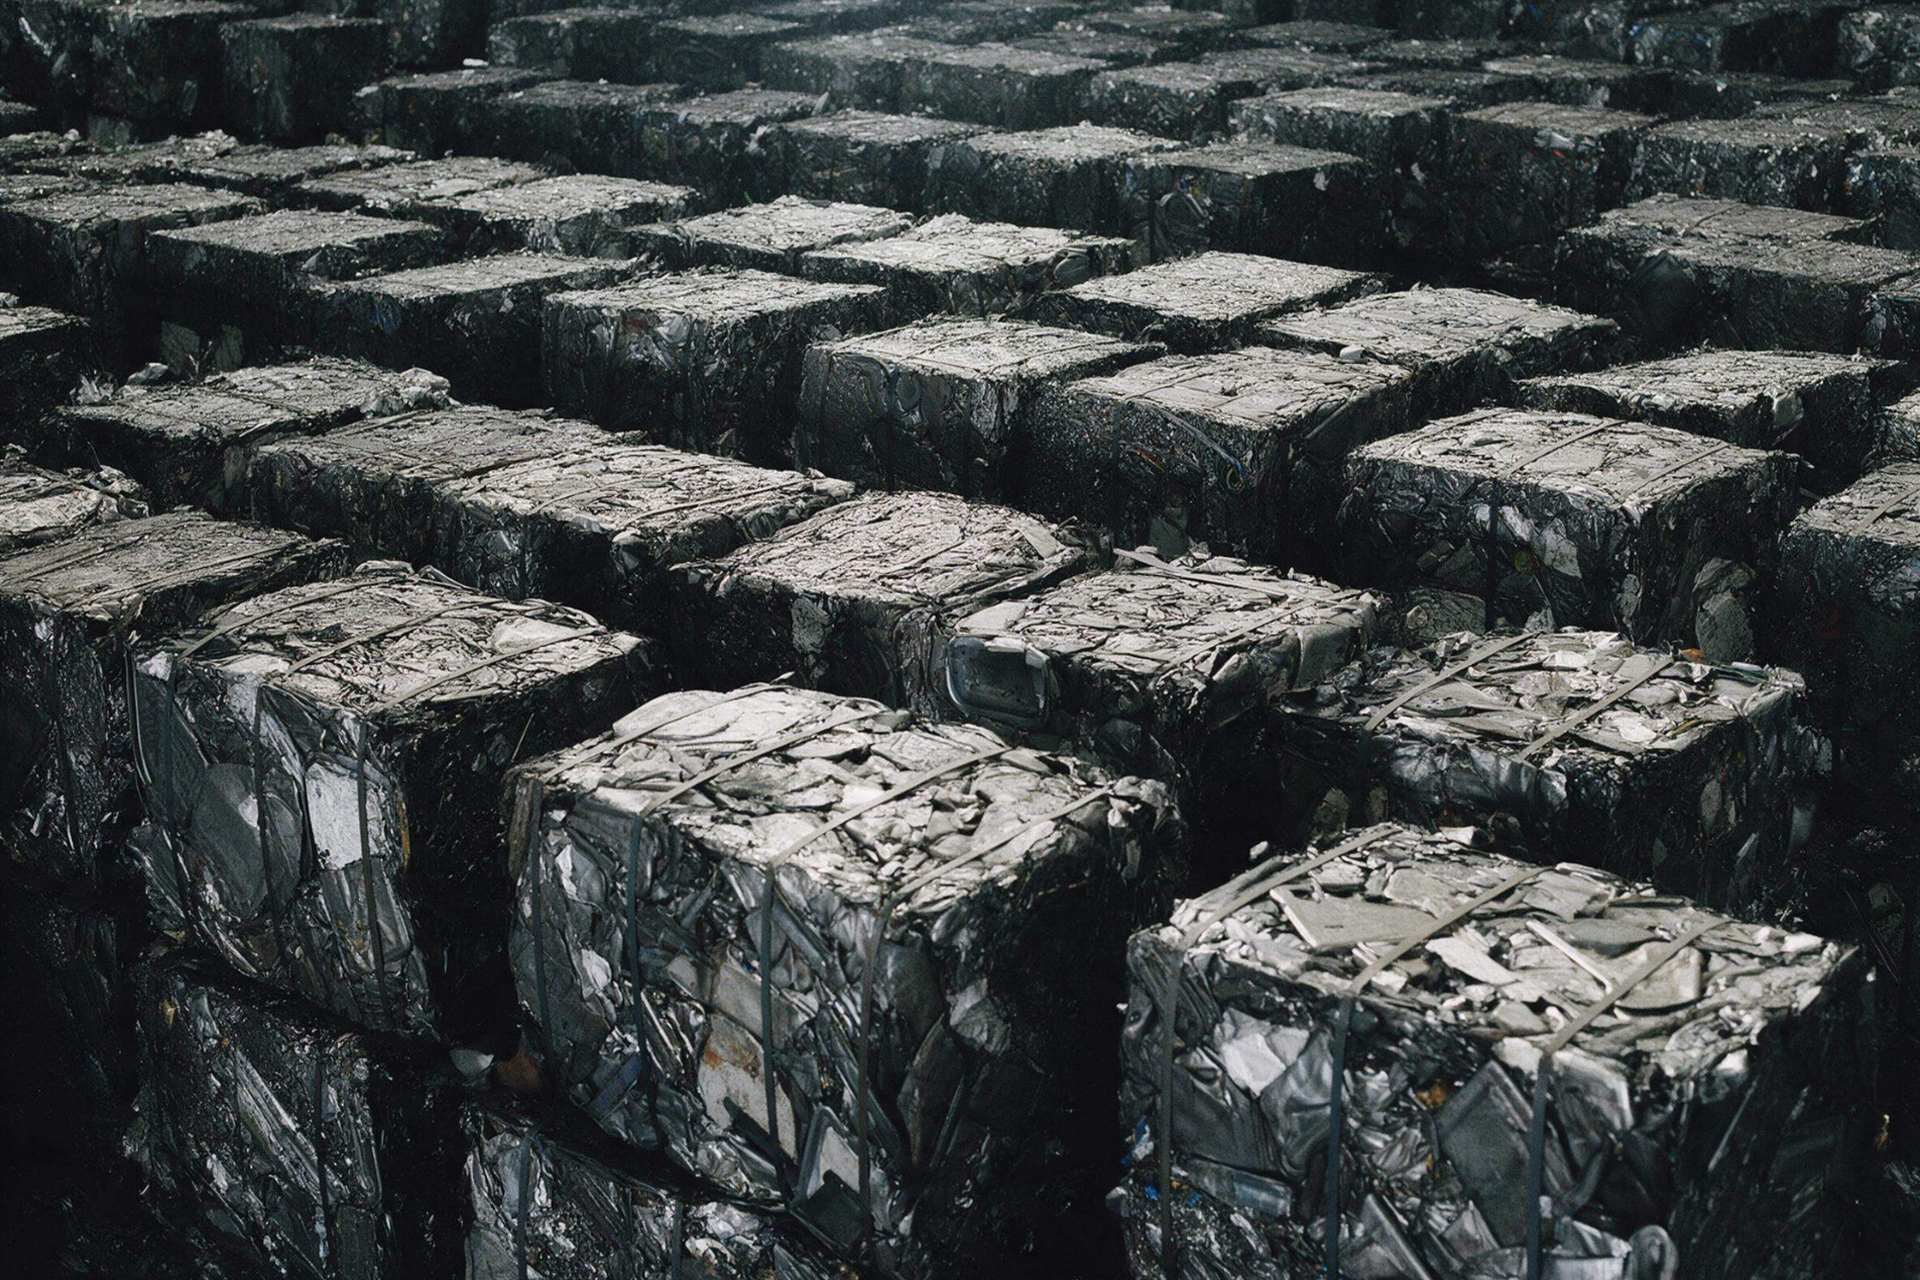
In Morocco, the paper, cardboard and printing industry supplies entire sectors: food producers that pack their goods, distributors that ship parcels, publishers and advertisers that print their materials. Paper mills, corrugated board plants, printing houses and converting workshops run heavy lines, often continuously, where metal is everywhere: machine frames, cylinders, dryers, conveyors, reels and storage structures. When a line changes, a workshop moves or a plant closes, this equipment becomes a significant metal resource, provided it is dismantled, sorted and cleared away methodically.
For plant directors, maintenance managers and workshop supervisors, the issue is not only freeing up space. Production continuing next door must be protected, risks linked to dust and inks must be prevented, and each part must be judged: what can be reused, and what belongs to material recovery. This guide explains, in practical terms, how to approach scrap metal from this industry in Morocco, from paper machines to printing presses.
What the paper, cardboard and printing industry covers
The industry brings together three complementary trades, often located in the same industrial zones around Casablanca, Tangier, Kenitra or Agadir. Paper mills prepare pulp, run the paper machine, dry the sheet, reel it and sometimes coat or treat it. Corrugated board plants turn paper into board: the corrugator makes the sheet, then converting lines cut, flexo-print, fold, glue and palletise the boxes. Printing houses and converting workshops, finally, print by offset, flexography, gravure or digital methods, then finish the work: guillotines, folders, binders, laminators and packing lines complete the chain.
Around the production lines, other metal equipment deserves the same attention: conveyors and transfers, silos and tanks, warehouse racks and shelving, handling trucks and trolleys, compressed-air and steam networks, electrical cabinets, and the maintenance workshops themselves, with their lathes, milling machines and spare-parts stocks. A complete inventory, workshop by workshop, is the starting point of any successful intervention.
Paper machines, corrugators and presses: heavy frames to dismantle by assembly
A paper machine is a long, heavy assembly: headbox, forming table, press section, dryer section made up of a battery of dryer cans, then the reel. Its frames are often cast iron and steel, its supporting structures massive, its walkways and handrails numerous. Dismantling cannot be improvised: it follows the reverse order of assembly, assembly by assembly, with marking, photographs and fasteners kept, so that every element can be identified and routed correctly.
Corrugators follow the same logic. A single-face or double-face corrugator combines heavy frames, fluted rolls, steam-heated rolls, tension frames and gluing systems. Printing presses, for their part, combine single-piece frames, print units, inking and dampening systems, dryers and unwind-rewind units. In every case, cutting to transportable sizes only happens after removable parts have been taken off and circuits drained. This method follows the same principles as industrial machine dismantling, applied here to lines where every hour of downtime counts.
Cylinders, rolls and precision parts: the sorting that makes the difference
Cylinders and rolls hold the greatest metal variety in the industry. They include cast-iron dryer cans, chrome-plated cylinders, ceramic anilox rolls, copper-plated engraved cylinders for gravure, rubber-covered rolls, as well as shafts, bearings and housings. Each family must be identified before cutting: a chrome cylinder is not handled like an ordinary steel roll, and a gravure cylinder deserves separate sorting, as in well-organised copper recovery in Morocco.
Alongside these parts are electric motors, gearboxes and drives, whose recovery of used electric motors follows its own rules, as well as stainless steel from the wet end — tanks, piping, pumps and fittings in contact with pulp — aluminium from housings and walkways, and copper from wiring and cabinets. Non-metallic coatings — ceramic, surface chrome, rubber, felts and wires — must be separated from the metal bodies so they do not degrade the batches. Finally, precision parts still in good condition — a regrindable cylinder, a straight shaft, a reusable bearing — must be assessed for reuse before any cutting, because a part destroyed too quickly is a part lost to an identical line.
Dust, inks and solvents: safety before cutting
The strongest feature of this industry is the risk linked to dust. Fine, combustible paper and board dust builds up on frames, inside ducts and around lines. Before any hot cutting, the areas concerned must be cleaned and vacuumed, build-ups removed, and a hot-work permit put in place with the plant safety manager. Cutting with a torch in a dusty workshop, without preparation, is the mistake that must never happen.
Inks, varnishes, glues and cleaning solvents need separate preparation. Inking circuits and tanks are drained, residues packed in closed, labelled containers and routed to suitable streams. The same applies to hydraulic oils and machine lubricants, drained before dismantling. Non-metallic parts — press felts, forming wires, belts, seals and gaskets — are separated from metals at removal, so they do not contaminate the batches. Coordination with the plant hygiene and safety service, ventilation of premises and fire-fighting equipment on site are an integral part of the works, not a formality added afterwards.
Line change, relocation and plant shutdown: phasing without stopping production
In a paper mill or board plant, production often continues while a neighbouring line is removed. Phasing is therefore the central tool: advance inventory, marking of assemblies, removal order — peripherals first, utilities next, main line last — and planned shutdown windows for work requiring a shared utility to stop, such as a steam supply or an electrical network. Each phase ends with the area restored: floors cleaned, access cleared, guards put back.
Clearance follows the same discipline. Removed metals are gathered on storage areas set away from production flows, without blocking reel reception docks or box shipments, then loaded onto suitable vehicles, carefully secured. For a relocation, dismantling must stay reversible: assemblies marked, plans kept, fragile parts protected, so the line can be reassembled in the new workshop. For a permanent shutdown, phasing workshop by workshop frees surfaces gradually, without paralysing the site. Agricultural scrap and data-centre scrap show the same phased approach in other Moroccan industries.
Reuse, spare parts and material recovery
Not every metal item leaving a paper mill, board plant or printing house automatically becomes scrap. A regrindable cylinder, a motor still working, a complete conveyor, a rack or an electrical cabinet in good condition can find a second life, either on an identical line or as spare parts for maintaining other sites. This reuse extends the life of equipment and avoids manufacturing new machines for needs that second-hand equipment can cover.
Conversely, a cracked, warped, deeply corroded part, or one that has become incompatible with current lines, must leave the reuse circuit and join material recovery, sorted by type: steel, cast iron, stainless steel, aluminium, copper and cables. The decision is taken at removal, by people able to judge the real condition of the part, not after prolonged storage in which batches become mixed. To understand the general framework of these interventions, the metal recycling in Morocco page presents the recovery streams, and the scrap metal purchase page sets out the collections organised by MOUMETAL for professionals.
FAQ — Paper, cardboard and printing industry scrap metal in Morocco
Can a paper machine be removed without stopping the whole plant? Yes, in many cases, provided work is phased, the removal zone is isolated, shutdowns of shared utilities are coordinated with production, and work on shared networks only takes place during planned windows. Feasibility depends on the layout of the line, its connections and production constraints.
What should be done with chrome or engraved cylinders at end of life? They should first be assessed for reuse or regrinding: a cylinder still straight and free of major defects can find a second life. Otherwise they are sorted separately from other steels, because their coatings and, for gravure, their copper layer require a specific route.
Why does paper dust require precautions before cutting? Because fine paper and board dust is combustible and can ignite on contact with a spark or flame. Cutting areas must therefore be cleaned and vacuumed beforehand, and hot cutting governed by a hot-work permit and suitable supervision.
How should remaining inks and solvents be handled before collection? Inking circuits and tanks are drained, residues packed in closed, labelled containers and routed to suitable streams. No liquid must remain inside a machine when it is cut or loaded.
Can a corrugated board line be relocated rather than dismantled for recovery? Yes, when the line is still in working order: dismantling is then reversible, assembly by assembly, with marking, protection of fragile parts and plans kept, so the line can be reassembled in the new workshop.
Entrust your paper mill, board plant or printing house scrap to MOUMETAL
MOUMETAL supports paper mills, corrugated board plants, printing houses and converting workshops with the removal, sorting and recovery of metals from their lines, from paper machines and corrugators to presses and cylinders. To organise an intervention, a site visit or a collection coordinated with your production, contact MOUMETAL on +212 660 690 806 or by email at contact@moumetal.com.